A thin wall can look simple in CAD and still become one of the hardest features to hold after machining. As stock is removed, the remaining section loses stiffness. Cutting force, clamp pressure, local heat and residual stress can then move the wall during the operation or after the part is released.
The practical objective is not to eliminate every micrometre of movement at the machine. It is to create a stable process in which the part reaches its required condition after unclamping, temperature equalization and inspection. That requires the drawing, stock condition, fixture and toolpath to be planned as one system.
Key Takeaways
- Thin walls deflect under tool pressure and can spring after unclamping.
- Balanced stock removal is usually safer than finishing one side while the opposite side remains heavy.
- Clamping force should locate the part without using the wall as a structural stop.
- A semi-finish allowance and a controlled rest period can reveal movement before final cuts.
- Critical dimensions should be inspected in the same supported or free-state condition defined by the drawing.
Why Thin-Wall Aluminum Parts Move
Wall deflection is only one source of error. Rolled plate, extruded stock and saw-cut blanks may contain residual stress. Removing material changes the internal balance, so a part that measures correctly in the fixture can bow when released. Uneven heat input and aggressive clamping add more movement. See our 6061 aluminum CNC machining guide.
The risk rises with long unsupported spans, deep pockets, interrupted walls and designs that remove most of the original blank. A single minimum wall-thickness number cannot predict success because wall height, alloy, temper, tool access and tolerance all matter.
Plan Workholding Around Datums, Not Around Clamp Pressure
A fixture should establish the functional datum surfaces and support the load path created by cutting. Soft jaws, sacrificial tabs, vacuum fixtures or custom nests may be considered according to geometry. The best option is the one that resists cutting force while leaving the required tool access. See our custom CNC milling services.
Avoid locating directly on a flexible wall unless the drawing intentionally uses that surface as a datum. Where support is temporary, its removal should be included in the process plan so the final free-state geometry can be checked.
Use a Balanced Roughing and Finishing Sequence
Rough opposing regions in stages instead of completely opening one side first. Leave a consistent semi-finish allowance, reduce radial engagement as stiffness falls and use sharp tools with reliable chip evacuation. A short tool and stable holder help reduce force and chatter. Sandvik Coromant’s thin-wall aluminum milling example provides useful process context for evaluating cutter engagement, wall support and remaining stock together.
For distortion-sensitive parts, allow the component to rest after heavy roughing or use an agreed stress-relief route before final machining. The need for stress relief depends on alloy, temper, blank history and tolerance, so it should not be added automatically.
Design Features That Can Be Machined and Measured
Increase internal radii where function allows, avoid unnecessarily deep narrow pockets and provide enough material near threaded inserts or fastening features. A rib may improve stiffness, but it can also trap a cutter or create a thick-to-thin transition. Review the complete geometry rather than applying a generic wall rule.
On the drawing, identify functional datums and critical wall relationships. Do not apply a tight profile or flatness tolerance to every surface when only a local interface controls assembly. See our internal corner radius in milling.
Inspect After the Part Reaches a Stable Condition
Inspection immediately after cutting may mix thermal change with actual process variation. Let the part reach the agreed inspection temperature and remove fixture force unless the drawing specifies a restrained condition. Flexible walls may require a defined support method so repeated measurements are comparable.
For production, record the first-off condition, fixture revision, tool life limit and measurement method. That evidence is more useful than a single isolated dimensional result.
A Practical Supplier Review Checklist
- 3D model plus a 2D drawing for controlled features
- Alloy, temper and preferred stock form
- Functional datum scheme and free-state or restrained inspection condition
- Wall profile, flatness and position requirements that affect assembly
- Quantity, finish and whether repeat workholding is expected
How Thin Can an Aluminum Wall Be?
The thinnest walls we have machined are about 0.8 mm. Whether a wall that thin is practical depends less on the thickness itself than on how tall and unsupported it is:
- Wall height to thickness: as a rough guide, keep unsupported walls below about 10–15 times their thickness. A 1 mm wall 10 mm tall machines well; the same wall 30 mm tall will vibrate and spring.
- Support: a wall connected to a floor and two corners is far stiffer than a free-standing fin.
- Tolerance: tight flatness or position on a thin wall is much harder to hold than the thickness itself.
- Material: 6061-T6 and 7075-T6 plate are common choices; stress-relieved plate moves less after roughing.
When a wall is thinner than it needs to be for function, our DFM review usually suggests making it thicker, which reduces vibration, scrap and machining time.
A Worked Example: Finned Aluminum Housing
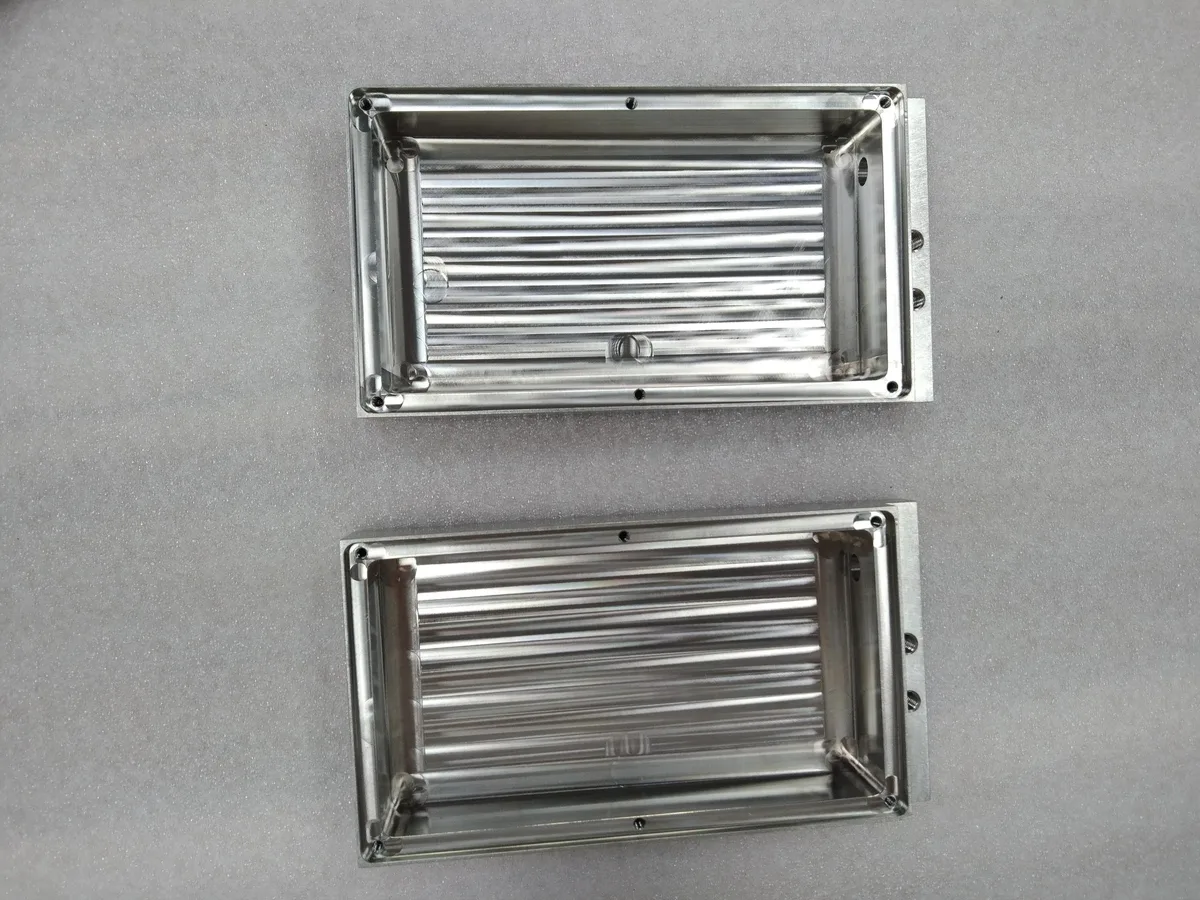
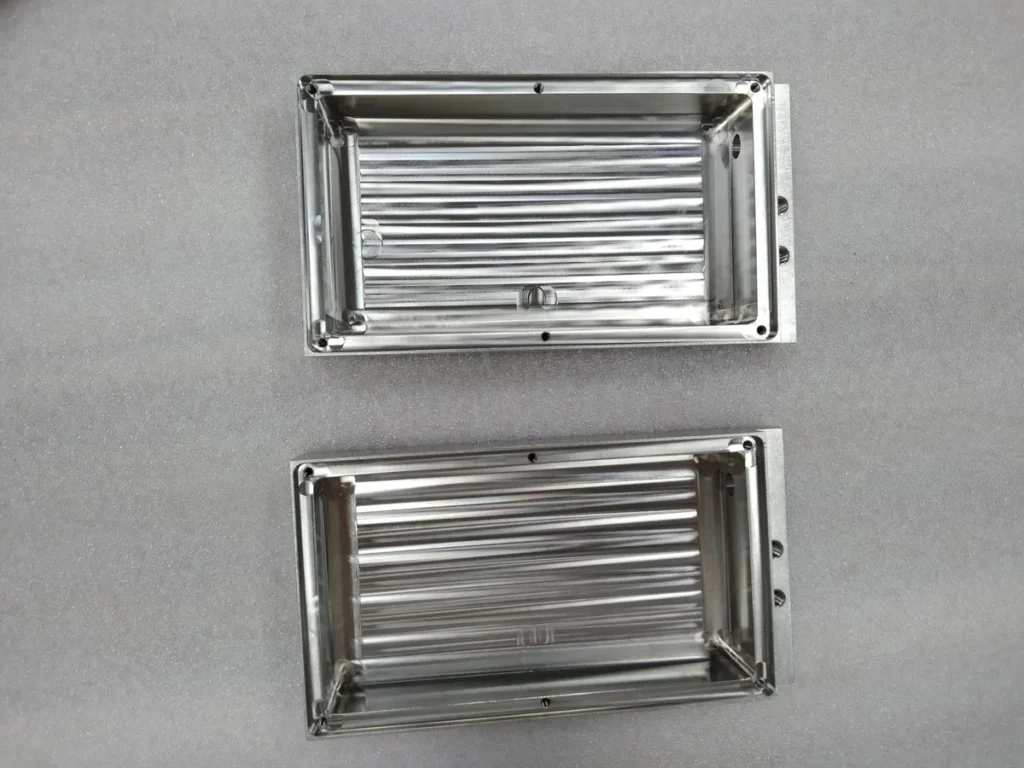
The housings below are aluminum heat-sink enclosures with a row of thin fins inside and walls of about 2 mm. A typical process for this kind of part:
- Rough the outside and the cavity in stages, leaving even stock on all walls so stress is released gradually.
- Release and re-clamp the part lightly before finishing, so it is not held in a strained shape.
- Finish the fins and walls with sharp, small-diameter tools, short stick-out and light radial cuts, alternating sides so each fin is cut while its neighbors still support it.
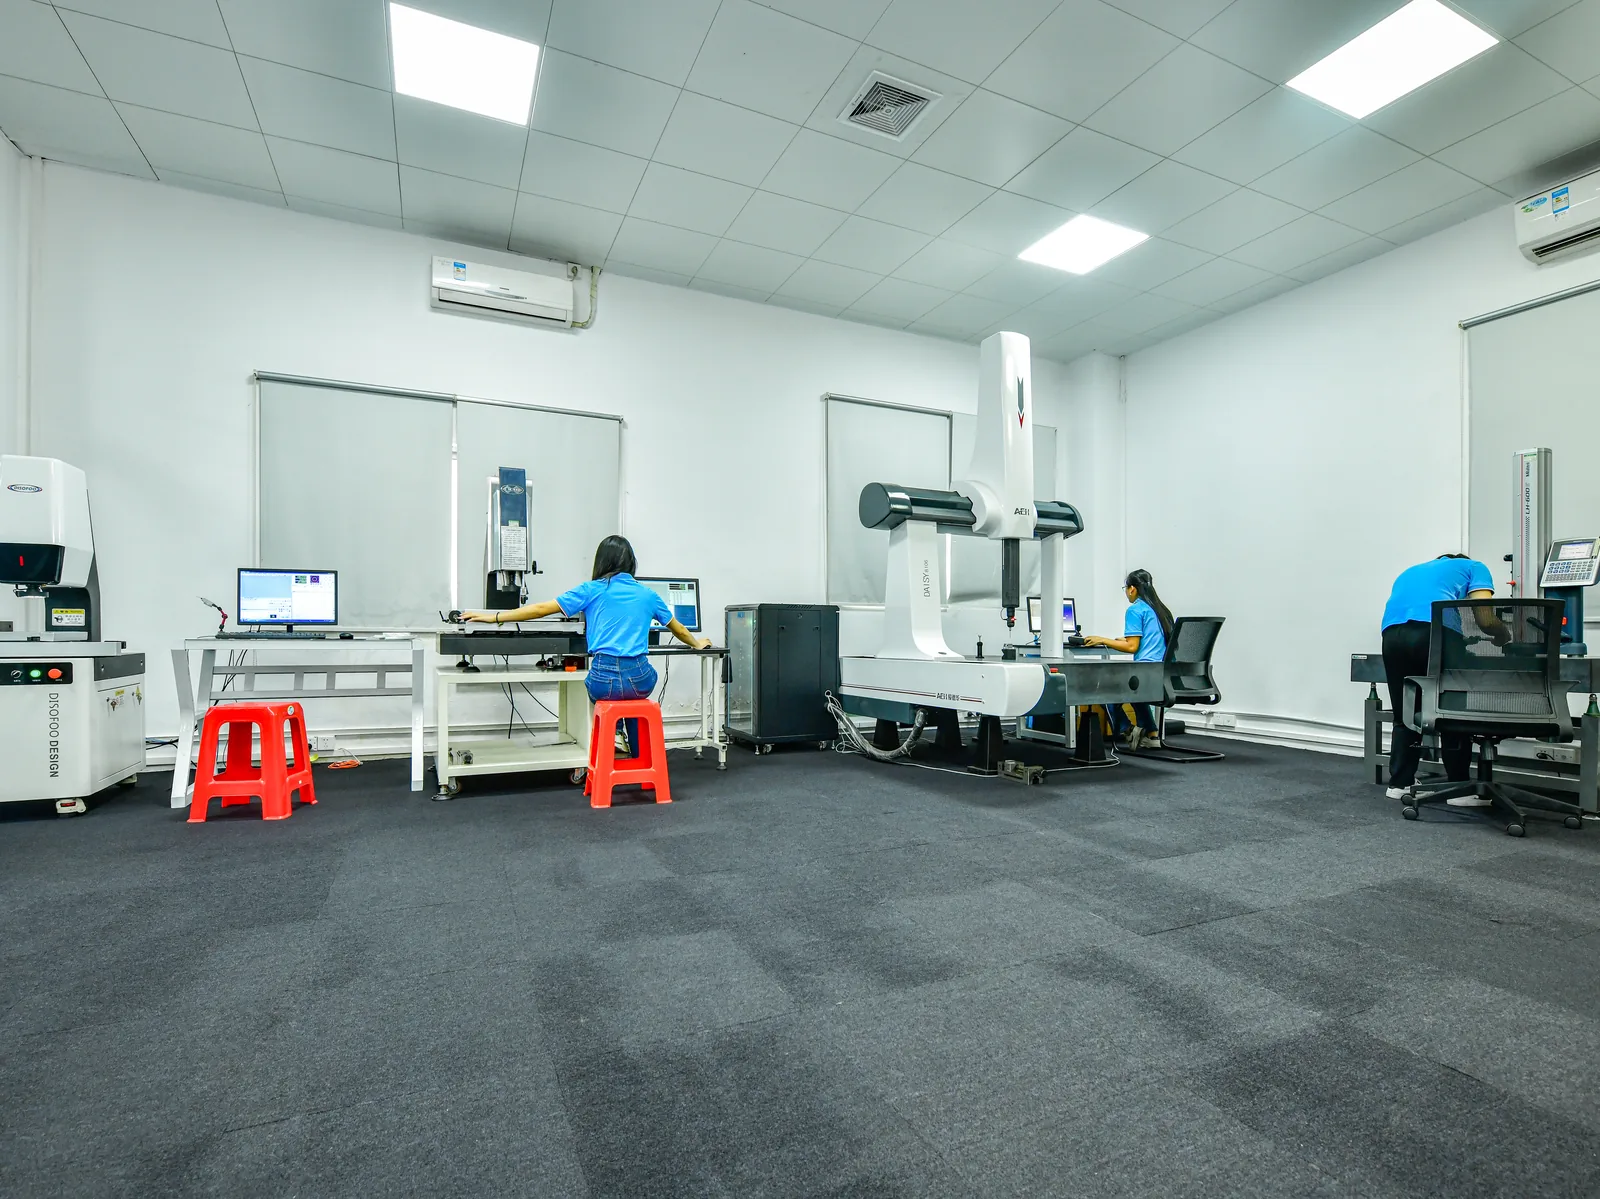
- Inspect after the part has cooled and is unclamped, with flatness of the sealing face checked on the CMM.
The fins are where most of the machining time goes. Slightly thicker fins or a larger spacing between them would cut machining time noticeably while hardly changing heat dissipation, which is a typical DFM suggestion for this kind of design.
What Drives the Cost of Thin-Wall Parts
- Wall height-to-thickness ratio, which sets how light the finishing cuts must be.
- Number of thin features, such as fins and ribs, each needing several light passes.
- Flatness and position tolerances on flexible walls.
- Custom fixtures or support material needed to hold the part without distortion.
- Stress-relieved or premium plate for parts that must stay flat.
- Inspection in a free state, which can take longer to set up.
See our CNC machining cost guide, and for deep cavities next to thin walls see our deep pocket guide.
Frequently Asked Questions
Can a thin wall be machined to a tight tolerance?
Often yes, but feasibility depends on wall height, support, material condition, datum strategy and measurement method. The tolerance must be reviewed against the complete geometry.
Should the part stay clamped during inspection?
Only if the drawing or inspection agreement defines a restrained condition. Otherwise, clamping can hide springback.
Does 7075 distort less than 6061?
Alloy choice alone does not determine distortion. Temper, stock history, geometry and material removal pattern can be more important.
Is stress relief always required?
No. It is a project-specific decision based on stock condition, material removal and final tolerance.
What is the minimum wall thickness for CNC machined aluminum?
About 0.8 mm is the thinnest we have machined, on short, well-supported walls. For general designs, 1.5–2 mm is a safer starting point.
Why does a thin part bend after it is unclamped?
Internal stress in the plate is released as material is removed, and clamping force may hold the part in a strained shape. When the clamps come off, the part moves to its free shape.
Is a thin-walled part cheaper because it uses less material?
Usually not. For CNC parts, machining time is the main cost, and thin walls need slower, lighter cuts. Thicker walls are often cheaper to machine.
Get an Engineering Review
Need a thin-wall aluminum part reviewed before production? Upload the 3D model, drawing, material and quantity so the machining and inspection route can be evaluated together. When the model and drawing are ready, use request a CNC machining quote and include the material, quantity, finish and inspection requirements.
For a review of CNC machining thin-wall aluminum, send the native CAD model, controlled drawing, material specification, quantity, finishing route and required acceptance records. SAMSHION’s engineering team can return project-specific DFM questions and documented quotation assumptions before production begins.