A hole can pass a diameter check and still fail in assembly. It may be out of position, tapered, not square to its datum, too rough for a seal or too tight after coating. Drilling, reaming and boring solve different parts of that problem, and the right choice starts with what the hole has to do.
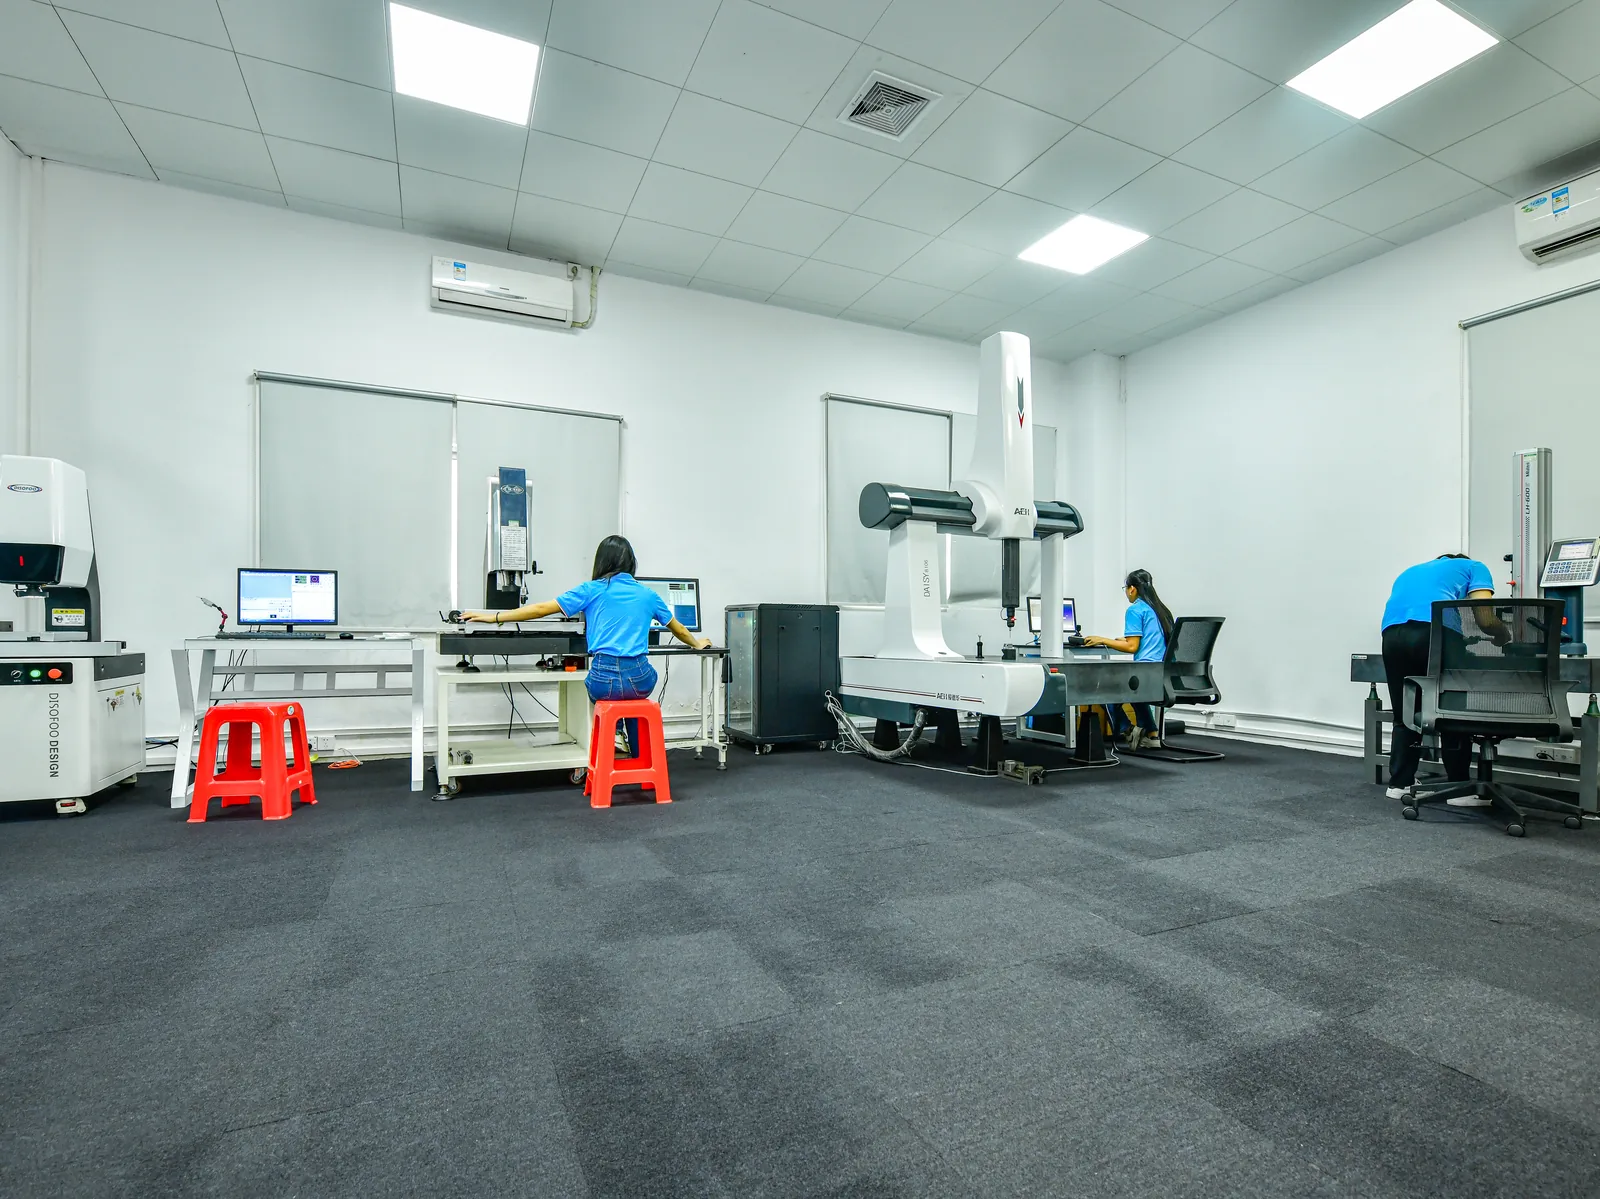
At SAMSHION we machine holes every day across 137 in-house CNC machines, from simple clearance holes to precision bearing bores, and we inspect them with plug and pin gauges, bore gauges and CMM. This guide explains how to specify a hole, when each process makes sense and how hole tolerances are checked. For the full service, see our CNC machining services. For standard tolerances by process, see our CNC machining tolerance chart.
Define What the Hole Must Do
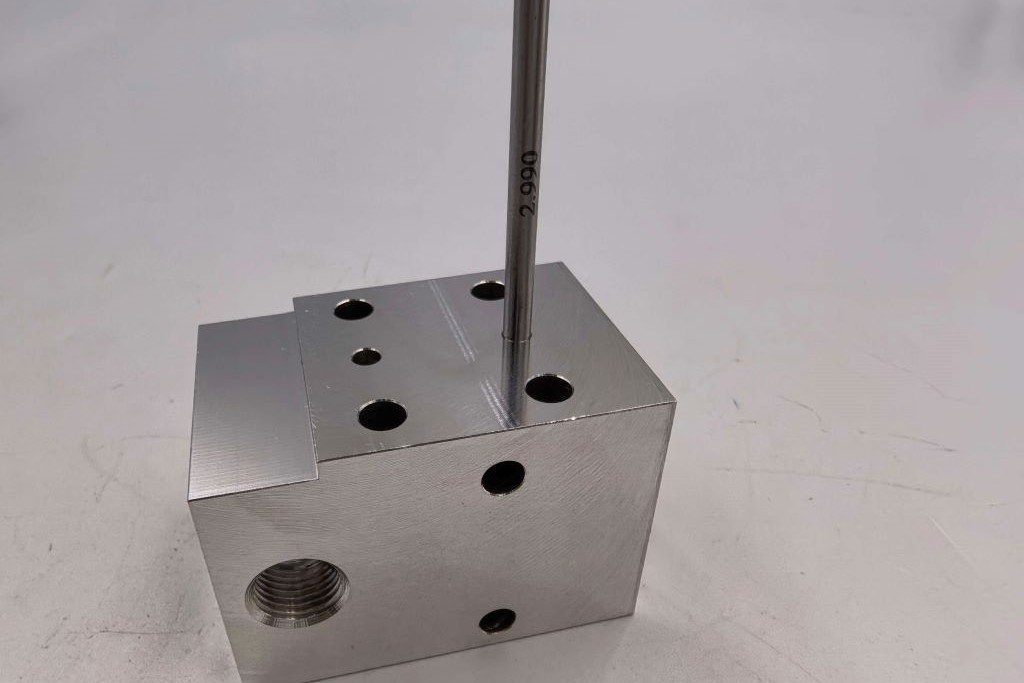
A clearance hole, a dowel hole, a bearing seat, a hydraulic passage and a tap drill hole do not need the same controls. Start with the mating part and the failure that matters: a dowel depends on position and fit, a bearing seat on size and roundness, a fluid passage on edge condition and cleanliness.
Tie the hole to datums that represent the assembly. A tight diameter tolerance cannot make up for an uncontrolled position. Untoleranced holes follow ISO 2768-mK by default, which we confirm with each customer; see our ISO 2768 tolerances chart. For precision pin holes, see our guide to dowel pin holes.
Drilling: Fast, but Usually Not the Final Size
Drilling creates the hole efficiently. Its final size and straightness depend on drill geometry, runout, material, depth and the entry surface. A drill can wander on an angled or uneven surface, or where it breaks into another hole. If the drilled condition is good enough for the function, there is no reason to add a finishing operation. If it is not, the hole is drilled undersize and finished by reaming or boring.
Deep holes need their own review for chip evacuation, straightness and tool reach; see our guide to deep hole drilling.
Reaming: Accurate Size on a Good Pre-Hole
A reamer removes a small, controlled amount of material to bring a drilled hole to size and improve its finish. It is efficient for repeated holes with tight diameter tolerances, such as dowel holes. A reamer follows the existing hole, so it does not correct a hole that was drilled in the wrong place or at an angle. Cross holes, interrupted bores and blind bottoms affect chip flow and tool support and need extra attention.
Boring: Correcting Size and Position
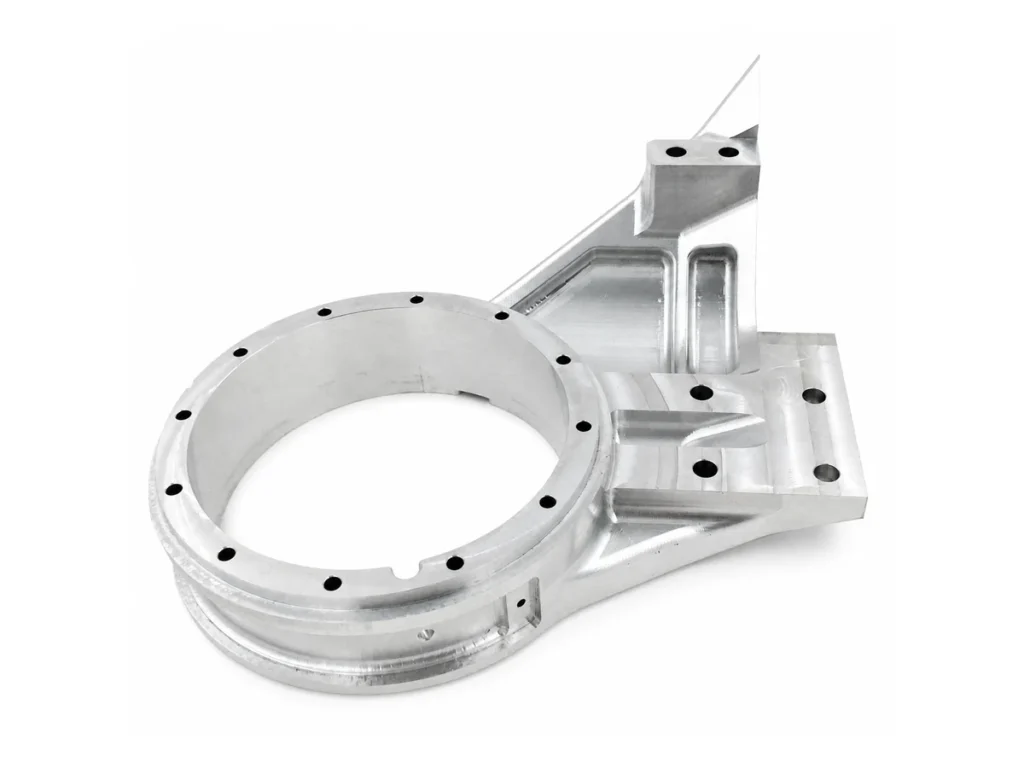
Boring uses a single-point tool to enlarge and finish a hole. Because the tool cuts the hole on the machine’s own axis, it can correct position and alignment as well as size, which makes it the usual choice for bearing seats and large precision bores. The boring bar must be stiff enough for the depth; a long overhang can cause taper or chatter. Larger holes can also be finished by circular interpolation with an end mill. Our robotic arm joint article shows how bearing bores are controlled for size, position and perpendicularity.
How Hole Tolerances Are Inspected
- Plug and pin gauges: fast go/no-go checks for diameter, used at the machine and in final inspection.
- Bore gauges: actual diameter values, measured at several depths to reveal taper.
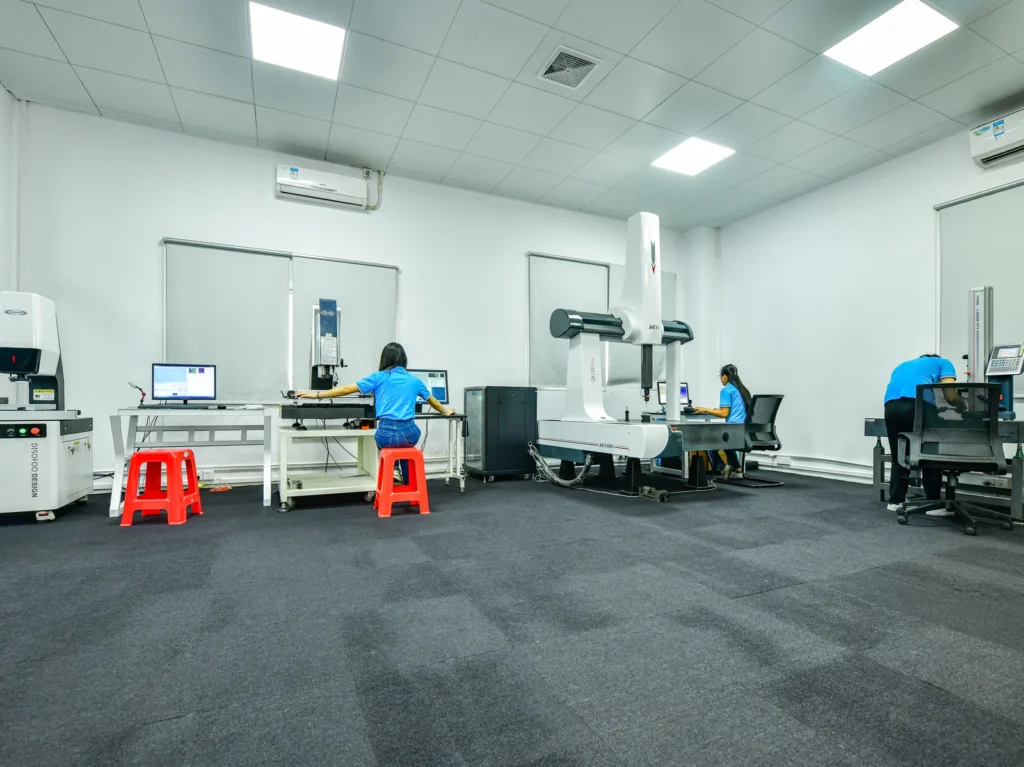
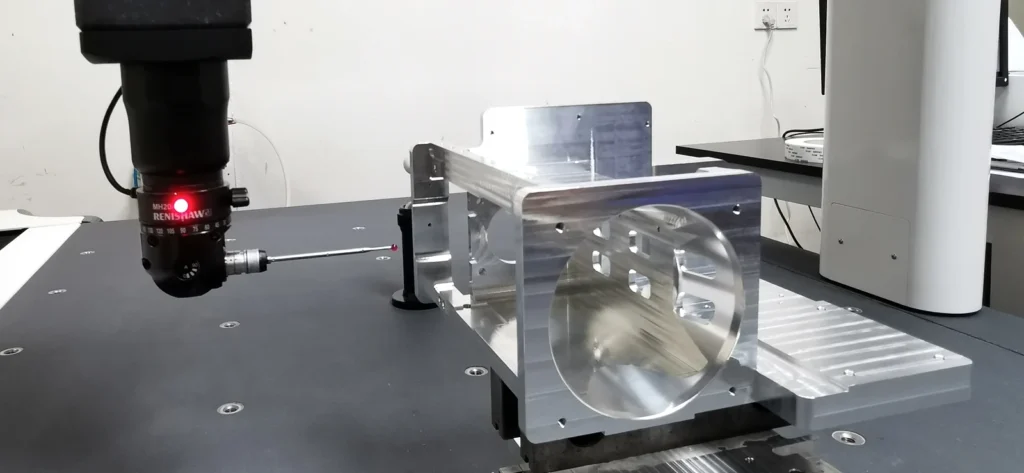
- CMM: position, perpendicularity, roundness and cylindricity relative to datums. Any GD&T requirement on a hole is checked on the CMM.
- Thread gauges: tapped holes are checked with go and no-go thread plug gauges; see our CNC threads guide.
State on the drawing or purchase order whether you need actual values, pass/fail results or a full first article report. See our quality assurance page for inspection equipment.
Common Hole Problems and Their Usual Causes
- Correct diameter, wrong position: drill wander, a reamer following a mislocated pilot, or a datum setup that does not match the drawing. Boring, or spot drilling before drilling, usually fixes it.
- Taper in a deep hole: tool deflection or chip packing. It needs better chip evacuation, a stiffer tool or a staged process.
- Out of round: a two-point gauge can miss lobing. Roundness and cylindricity have to be checked on a CMM when the function depends on them.
- Tight after coating: anodizing or plating builds up on the bore. Agree whether the hole is masked, machined oversize or sized after coating.
- Burrs at entry or exit: they make a hole gauge tight and damage seals. Holes are deburred before they are gauged.
Hole Specification Checklist
- Hole function and mating part
- Diameter and tolerance, depth and bottom condition
- Position and orientation relative to datums
- Surface finish or sealing requirement
- Coating allowance and whether size applies before or after finishing
- Inspection method and report level
Request a Hole Tolerance Review
Send a 3D model and a 2D drawing with material, quantity, finish and inspection requirements. Our engineers will review hole function, process, coating allowance and inspection together before machining. Request a quote.
Frequently Asked Questions
Can a reamer fix hole position?
No. A reamer improves size and finish but follows the existing hole. Position errors are corrected by boring or by spot drilling and drilling accurately in the first place.
Is boring better than reaming?
They solve different problems. Reaming is efficient for repeated small precision holes on a good pre-hole. Boring corrects size and position and suits bearing seats and large bores.
How do you measure an H7 hole?
With plug gauges or bore gauges for size, and on a CMM when position, perpendicularity or cylindricity are specified.
Should coating be applied before final hole sizing?
It depends on the coating and the fit. Agree before machining whether the hole is masked, machined oversize or sized after coating.
What tolerance applies to holes without a tolerance on the drawing?
Our default is ISO 2768-mK, which we confirm with the customer before production.