304, 316 and 17-4 PH are all called stainless steel, but they are not equivalent. 304 and 316 are austenitic grades, while 17-4 PH is a precipitation-hardening stainless supplied and heat treated in defined conditions.
The correct choice depends on corrosion environment, mechanical load, temperature, magnetic response, welding, heat treatment and regulatory requirements. Machining strategy follows that material decision.
Key Takeaways
- 304 is a widely used general-purpose austenitic stainless.
- 316 adds molybdenum and is often chosen for improved resistance in chloride-related environments.
- 17-4 PH can provide higher strength after suitable heat treatment.
- Austenitic stainless can work harden when tools rub or dwell.
- State grade, product specification and heat-treatment condition on the drawing.
304 Stainless: General Fabrication and Machined Parts
304 combines corrosion resistance, formability and broad availability. It is common for food equipment, enclosures, fittings and general industrial components. Machining requires sharp tools, positive cutting action and reliable chip control. Published composition and property data can be checked in the World Stainless technical property tables, while the purchase specification must still state the exact grade, condition and certification required for the project.
It is not automatically suitable for every salt, chemical or high-temperature environment. Application review remains necessary. See our cast iron CNC machining guide.
316 Stainless: Additional Corrosion Resistance
316 contains molybdenum and is often selected where chloride exposure or more demanding corrosion conditions exist. It is common in marine, pharmaceutical, chemical and hygienic equipment.
Improved corrosion resistance does not remove the need for surface condition, passivation, crevice design and cleaning review.
17-4 PH: Strength Through Heat Treatment
17-4 PH can be machined and heat treated to defined conditions that provide different strength and toughness. The drawing must identify the required condition, because ’17-4′ alone does not define final properties.
Machining before or after aging changes tool load, distortion risk and final dimensions. The process sequence should be planned with the heat treater.
Machining Work-Hardening Stainless
Austenitic stainless can harden locally if the tool rubs instead of cutting. Stable engagement, sharp edges, sufficient feed and coolant delivery help avoid repeated cutting of a hardened layer. Long stringy chips also require control. See our CNC milling services.
Tool recommendations depend on machine, holder, operation and material condition, so avoid publishing universal speeds as fixed rules.
Finishing, Passivation and Inspection
Surface treatment may remove free iron or improve cleanliness, but it is not a repair for deep tool marks, embedded contamination or poor drainage design. Specify the applicable finish or passivation standard and whether weld heat tint must be removed.

Material certificates and heat-treatment records may be important for controlled applications. See our surface finishing services.
Stainless Selection Checklist
- Corrosion medium, temperature and cleaning chemicals
- Mechanical strength and heat-treatment condition
- Welding, passivation and surface finish
- Magnetic or vacuum requirements
- Material certification and traceability
Quick Comparison: 304 vs 316 vs 17-4 PH
- Composition: 304 is roughly 18 percent chromium and 8 percent nickel. 316 adds about 2 to 3 percent molybdenum and slightly more nickel. 17-4 PH contains about 15 to 17.5 percent chromium, 3 to 5 percent nickel and 3 to 5 percent copper, which allows precipitation hardening.
- Corrosion resistance: 316 is generally the best of the three in chloride environments such as seawater, de-icing salts and some cleaning chemicals. 304 is adequate for most indoor and general industrial uses. 17-4 PH is broadly comparable to 304 in many environments, depending on heat-treatment condition.
- Strength: annealed 304 and 316 have a minimum tensile strength of about 515 MPa. 17-4 PH in the H900 condition can exceed 1300 MPa, more than twice as strong.
- Hardness after machining: 304 and 316 cannot be hardened by heat treatment, only by cold work. 17-4 PH can be machined in a softer condition and then aged to the required hardness.
- Magnetism: annealed 304 and 316 are essentially non-magnetic but can become slightly magnetic after cold work or heavy machining. 17-4 PH is magnetic.
- Machinability: all three are harder to machine than carbon steel. 316 is usually the most difficult because it is gummy and work-hardens readily; 17-4 PH machines reasonably in the solution-treated condition but becomes harder after aging.
- Material cost: 304 is normally the least expensive, with 316 and 17-4 PH costing more because of their molybdenum, nickel and copper content.
Cutting Parameters and Tooling for Stainless
Most problems in stainless machining come from heat and work hardening. General practice that applies to all three grades:
- Use sharp carbide tools with a positive rake and a coating suited to stainless; replace tools before they are worn, because a dull edge rubs and hardens the surface.
- Keep the feed high enough that the tool always cuts beneath the hardened layer left by the previous pass. Light, hesitant cuts are the most common cause of rapid tool wear.
- Use lower cutting speeds than for aluminum, with plenty of coolant aimed at the cutting zone.
- Avoid dwelling, stopping in the cut, or re-cutting chips. Good chip evacuation is critical in deep pockets and drilled holes.
- Drill with through-coolant where possible and finish tight holes by reaming or boring.
- Tap with sharp, stainless-specific taps; for small threads in 316, thread milling or forming may be more reliable. See our guide to machining threads.
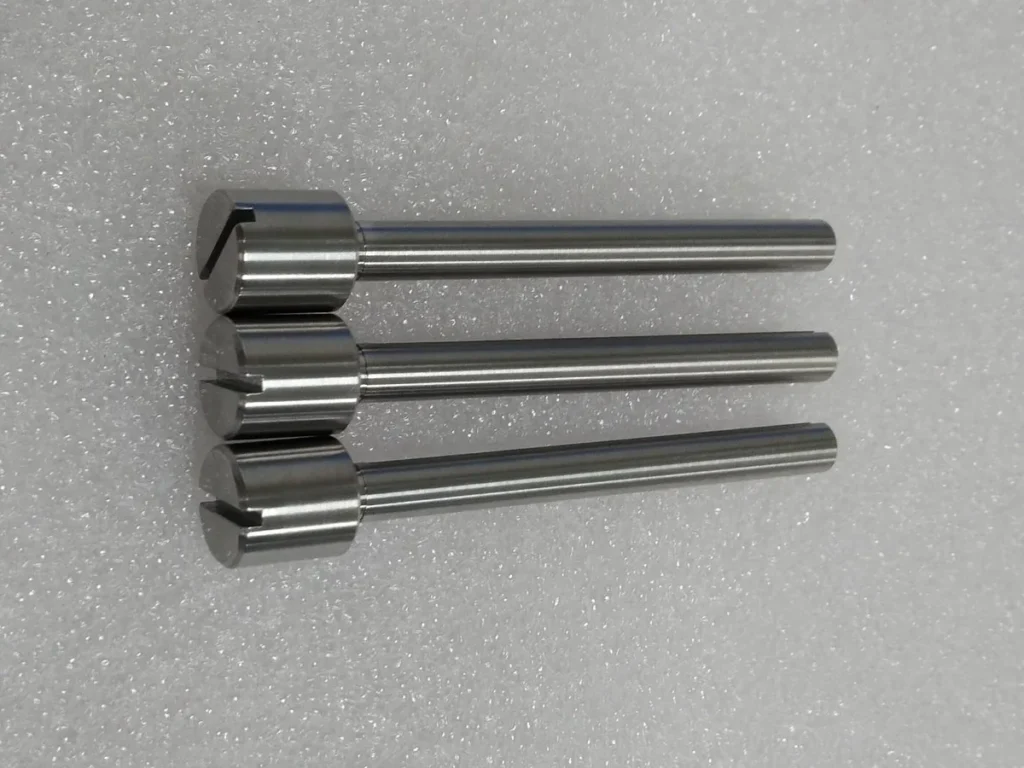
A Worked Example: Choosing a Grade for a Stainless Pin
Consider a small locating pin used in a piece of production equipment. The choice of grade depends on what the pin has to survive:
- If the pin works indoors, sees moderate loads and needs only to resist rust and handling, 304 is usually the economical choice.
- If the same pin is used in food processing equipment that is washed down with chlorinated cleaners, or near the sea, 316 is the safer choice because of its molybdenum content.
- If the pin must resist wear and carry high shear loads, 17-4 PH aged to a defined condition gives far higher strength and hardness while keeping reasonable corrosion resistance.
In each case the drawing should state the grade, the heat-treatment condition (for 17-4 PH) and any surface treatment, so the quote, the material purchase and the inspection all refer to the same requirement.
Verifying the Grade: Certificates and Spectrometer Checks
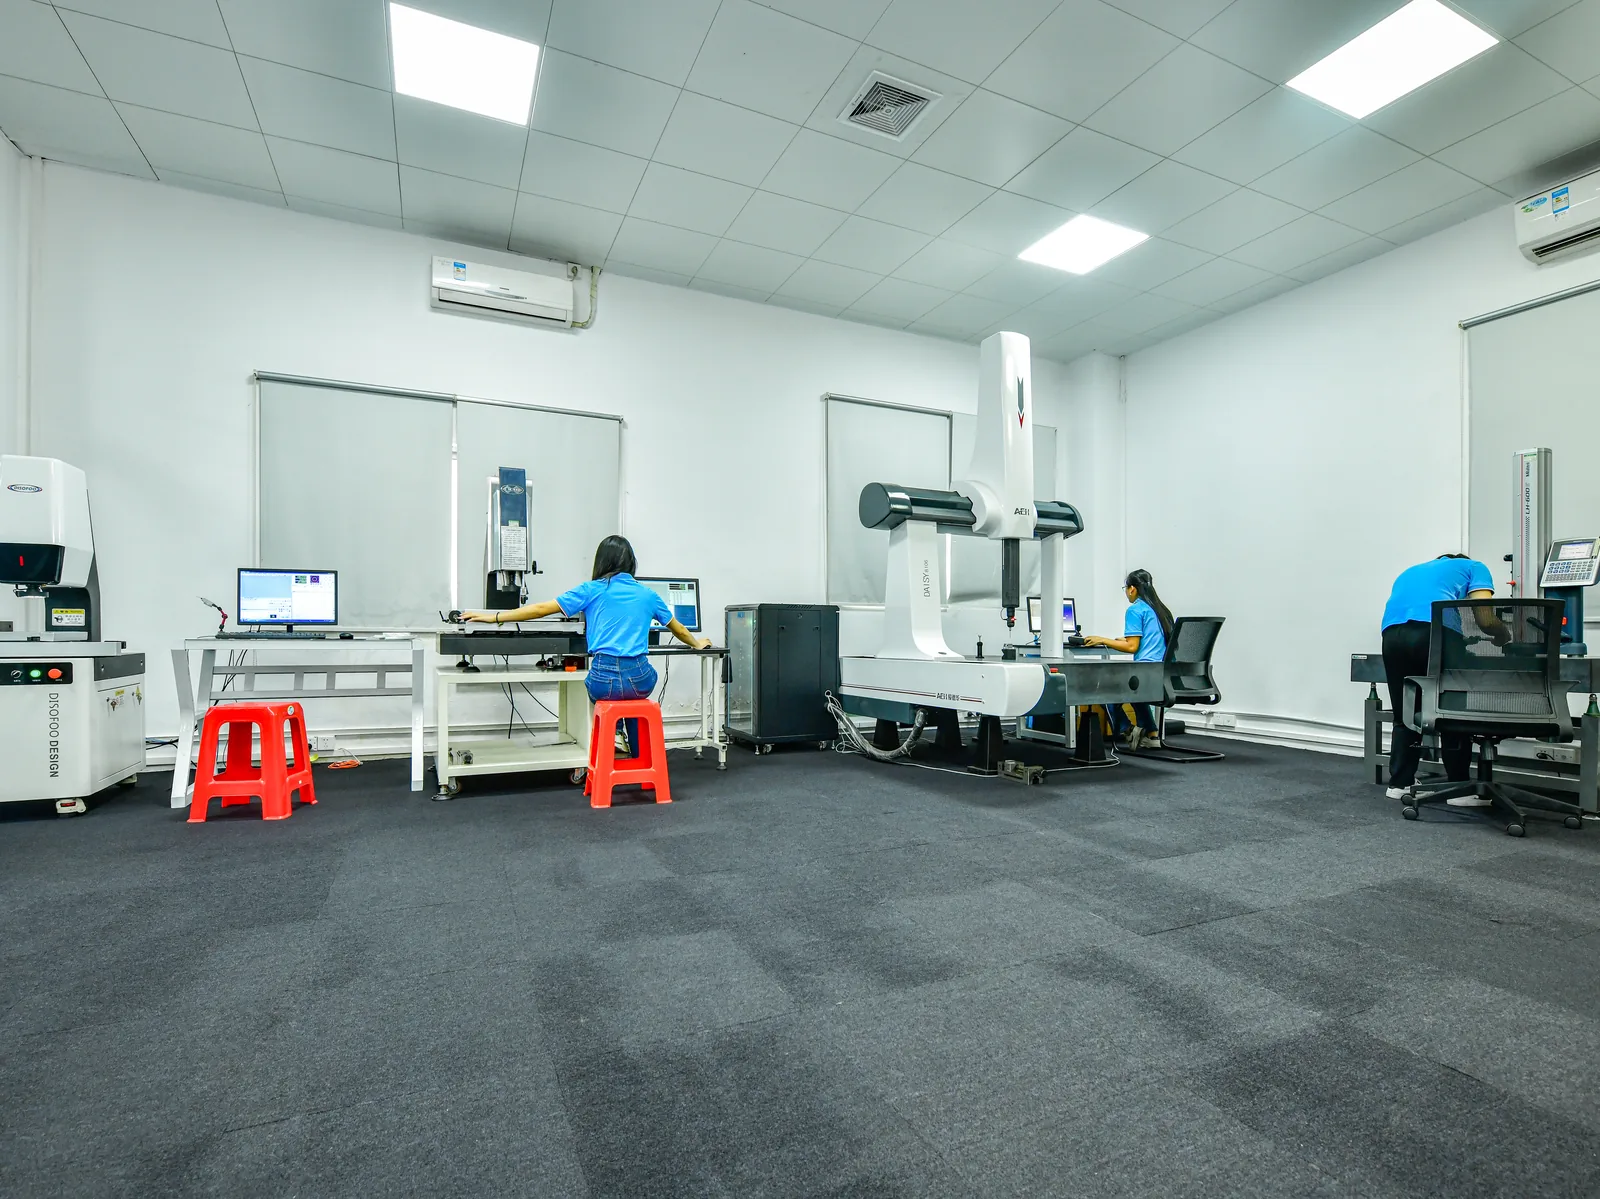
304, 316 and 17-4 PH look identical once machined, so mixing them up is a real risk. Material certificates from the mill or stockist are the first line of control. At SAMSHION we also use a handheld spectrometer to check alloy composition, which can distinguish 304 from 316 by detecting molybdenum before the material goes to the machine. This is especially useful when a part is critical for corrosion resistance and a mix-up would not be found until the part fails in service.
What Drives the Cost of Stainless Steel Parts
- Grade: 316 and 17-4 PH stock costs more than 304.
- Machining time: stainless is cut more slowly than aluminum, and tools wear faster, so cycle time and tooling cost are higher.
- Heat treatment: 17-4 PH parts need an aging step, and critical features may need finishing after heat treatment.
- Deep features and small threads: deep holes, narrow slots and fine threads are slower and riskier in stainless than in softer materials.
- Surface treatment: passivation, electropolishing or bead blasting add a process step and lead time.
- Certification: material certificates and traceability requirements add documentation work.
- Quantity: setup and programming are spread over the batch, so repeat orders cost less per part than one-off prototypes.
Common Mistakes When Specifying Stainless
- Writing only “stainless steel” on the drawing, leaving the grade to the supplier.
- Choosing 316 everywhere “to be safe”, which raises cost and machining time when 304 would do the job.
- Specifying 17-4 PH without the heat-treatment condition such as H900 or H1150.
- Expecting passivation to remove deep tool marks or contamination; it is a chemical cleaning step, not a repair.
- Assuming 304 and 316 are always non-magnetic; machined or cold-worked areas can attract a magnet slightly.
- Applying tight tolerances on every feature, which multiplies the time spent cutting a difficult material.
Frequently Asked Questions
Is 316 always more corrosion resistant than 304?
316 often performs better in chloride-related environments, but actual corrosion depends on concentration, temperature, design and surface condition.
Is 17-4 PH the same as 304 or 316?
No. It is a precipitation-hardening stainless with different heat-treatment and strength behavior.
Why does stainless machining create poor tool life?
Work hardening, heat, chip control, tool geometry and machine stability can all contribute.
Should stainless parts be passivated?
Only when the application and specification require it. The correct process depends on grade and prior operations.
Is 304 or 316 stainless magnetic?
In the annealed condition both are essentially non-magnetic. Cold work, bending or heavy machining can make local areas slightly magnetic, so a magnet test is not a reliable way to tell 304 from 316. A spectrometer check or material certificate is.
Can 303 be used instead of 304?
303 is a free-machining version of 304 with added sulfur. It machines faster and is often cheaper to produce, but it has lower corrosion resistance and poorer weldability. It is a good choice only when the application allows it and the drawing says so.
Which stainless grade is cheapest to machine?
Of the three grades in this article, 304 is normally the most economical in both material and machining time. 316 costs more and machines more slowly. 17-4 PH adds a heat-treatment step. See our CNC machining services for a quote based on your drawing.
Get an Engineering Review
Send the service environment, grade and condition, drawing and certification needs for a complete stainless-machining review. When the model and drawing are ready, use request a CNC quote and include the material, quantity, finish and inspection requirements.
For a review of 304 vs 316 vs 17-4 stainless steel, send the native CAD model, controlled drawing, material specification, quantity, finishing route and required acceptance records. SAMSHION’s engineering team can return project-specific DFM questions and documented quotation assumptions before production begins.